This content was written and submitted by the supplier. It has only been modified to comply with this publication’s space and style.
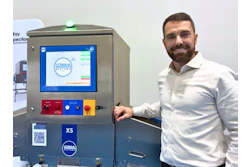
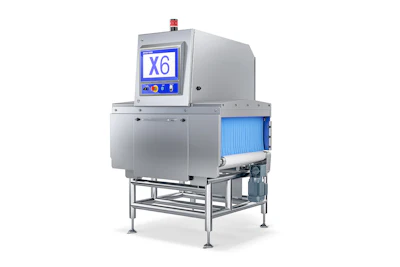
METTLER TOLEDO Product Inspection Group introduces the X56 DXD+ dual energy photon-counting x-ray inspection system with AI capabilities, expanding the innovative X6 Series portfolio. This system will be on display at PACK EXPO International in Booth S-2122.
Designed specifically for packaged applications, the X56 DXD+ enables manufacturers to inspect every product with confidence by delivering enhanced contamination detection capabilities. This makes the x-ray solution ideal for challenging applications where low-density contaminants, such as rubber and plastics must be reliably detected. Food manufacturers benefit from protecting brand integrity and supporting premium product safety in complex formats, such as pet food, potato chips or potatoes. The X56 DXD+ makes compliance with regulatory and retailer requirements easier to achieve.
The X6 Series now offers manufacturers a full range of x-ray inspection solutions to suit different product sizes, from individual packs to large cases or multi-packs. The X56 DXD+ builds on the success of the X16 and X36.2 systems and brings advanced dual energy photon-counting capabilities for medium to large-sized products on single lanes or smaller packages running across multiple lanes, in a 500mm system width.
AI Inspection for Enhanced Quality Checks
AI integration helps to improve the quality and reliability of quality inspection tasks while reducing unnecessary product rejection. This is beneficial to overcoming inspection challenges in complex scenarios like overlapping or mixed products thereby contributing to increasing production process efficiencies. The AI integration is not limited to the X56 DXD+; it is also available on other x-ray systems within the METTLER TOLEDO product range.
Built for High levels of Performance and Flexibility
Powered by DXD+ detector technology and Advanced Material Discrimination Pro (AMD Pro) software, the X56 DXD+ delivers exceptional performance for complex applications that conventional single energy systems may struggle with, particularly when detecting low-density contaminants in packaged products with high variability in thickness, density or overlapping textures, such as multi-packs, bags of crisps or bulkier cartons. This high level of detection sensitivity supports effective quality control, even in noisy or high-contrast products where conventional systems may fall short.
This makes the X56 DXD+ a powerful complement to the X6 Series. The X16 is positioned for inspecting single packages at high speed and the X36.2 is customizable for more advanced, high-throughput environments and is available for multi-lane inspections.
Smart Design for Speed & Productivity
The X56 DXD+ has been designed with operational efficiency in mind. The system combines premium detection performance with an intuitive interface, toolless belt removal for fast cleaning and a robust hygienic design suited to high-speed, high-volume environments. With throughput rates of up to 500 products per minute, the X56 DXD+ matches the demands of production lines, helping manufacturers boost efficiency and combat rising operational costs through enhanced productivity and intelligent design.
Through built-in product quality tools including completeness checks, clip detection and product trapped in seal inspection, the X56 DXD+ also supports effective quality control by enhancing consistency and protecting brand integrity beyond contamination detection alone.
Flexible Integration for a Global Market
Compatible with a wide range of conveyor heights and reject options, and available in single or multi-lane configurations, the X56 DXD+ has been developed as a global solution for manufacturers needing greater flexibility and performance. Its advanced software provides full traceability through a recorded image database, which can be accessed on-screen or integrated with METTLER TOLEDO ProdX™ data management software for centralized monitoring and compliance.
This connectivity, along with support for common network protocols, makes compliance easier by enabling real-time monitoring, secure record-keeping and simplified audit readiness across global production environments. ProdX™ automates the monitoring, reporting and collation of all inspection activities in real-time.
The securely stored data helps facilitate regulatory compliance, provides clear proof of due diligence to protect brand reputation and enables data-driven decisions that can lead to performance and productivity improvements across the line.
Chris Plant, Head of Market Management, METTLER TOLEDO, says, “The launch of the X56 DXD+ expands our X6 Series, offering a comprehensive suite of inspection solutions tailored to modern food manufacturing. With its dual energy photon-counting capabilities, the X56 DXD+ delivers new levels of detection performance in complex packages across single and multi-lane formats. This advanced inspection capability will further help customers inspect every product with confidence, protect productivity, brand reputations and profits, plus comply easily with industry requirements.”
Learn how the METTLER TOLEDO X56 DXD+ dual energy photon-counting system can transform inspection for your production line.
METTLER TOLEDO to Introduce M50 R-Series AdvancedLine Metal Detectors at PACK EXPO
 M50 R-Series AdvancedLine metal detector from METTLER TOLEDOMETTLER TOLEDO
METTLER TOLEDO Product Inspection Group introduces its M50 R-Series AdvancedLine metal detectors to North America at PACK EXPO Booth 2122. This advanced generation of metal detectors is designed to support food manufacturers facing increasing demands around compliance, traceability, data connectivity and line performance.
"The launch of the M50 R-Series reflects how closely we have listened to our customers. We understand the pressures that food manufacturers face every day: balancing productivity with growing expectations around compliance, traceability and digital connectivity. As production lines become faster and more complex, maintaining that balance becomes even more challenging," said Jaison Anand, Market Manager - Metal Detection at METTLER TOLEDO Product Inspection. "The M50 R-Series has been developed to help address these challenges, delivering advanced detection performance alongside intuitive operation and future-ready connectivity, supporting manufacturers not only today but as their requirements continue to evolve."
The M50 R-Series introduces a range of new innovations developed to increase detection sensitivity and support product safety across different applications. These include the eDrive PLUS, which, when combined with a 900 kHz frequency, improves the field strength to deliver the highest sensitivity to detect the smallest wire and non-spherical metal contaminants. Cutting-edge algorithms such as the 3S PLUS combined with AI-based machine learning help achieve maximum sensitivity, minimizing the risk of product recalls and helping manufacturers produce safer products.
Metal detectors in the series include:
- M55R – Optimized for detecting significantly smaller, irregularly shaped metal contaminants in dry products such as pasta, savory snacks and deep-frozen produce (where thawing does not occur).
- M55RB – Optimized for bulk products such as large sacks, bags of powder and cartons. Radio frequency interference (RFI) shields filter out external interference in large-aperture applications, increasing metal detection sensitivity. The innovative coil geometry delivers consistent detection performance in busy production environments.
- M56R – Optimized for challenging applications such as chilled, wet, dry, deep-frozen/thawing and metalized film-wrapped products. It incorporates multi-simultaneous frequencies, an enhanced 3S PLUS algorithm to minimize the active product signal and an AI-based machine learning process to improve sensitivity on wet or conductive products and virtually eliminate false rejects. The inclusion of a 900 kHz tuned frequency provides excellent performance on dry products, making it a highly versatile solution for manufacturers with diverse products on the line.
The M50 R-Series has been designed to maximize uptime and simplify daily operation. A new 10.1-inch capacitive touchscreen provides clear visualization and intuitive navigation. The interface responds like a smartphone or tablet screen, even when the user is wearing gloves or the screen is wet, to support faster setup and more confident use than traditional resistive touchscreens.
The introduction of the INFINITY Electronic Test System represents a significant advancement in routine testing. Automation in production performance monitoring simplifies test routines, improves consistency and accuracy and is up to three times faster than manual testing. The M50 R-Series can also run tests automatically without operator intervention.
Embedded Wi-Fi supports secure and simplified connectivity, giving users rapid access to system information through QR code functionality. Combined with improved Condition Monitoring software and simplified data transfer, the M50 R-Series supports continuous operation and reduced disruption on the line.
Brand protection is also enhanced through new radio-frequency identification (RFID) access control, which supports individual user logins and access management for superior security. Detailed access records are stored locally or transferred through multiple communication protocols, including OPC-UA and EtherNet/IP.
Manufacturers have the option to take product safety and data security to the next level by integrating ProdX™ data management software from METTLER TOLEDO. By connecting all METTLER TOLEDO Product Inspection devices, ProdX monitors and records all inspection activities in real time and safely stores the data indefinitely.